RO WATER TREATMENT
RO WATER TREATMENT
Products Description
Feature
1. Advanced RO Membrane Core for Efficient RO Water Treatment
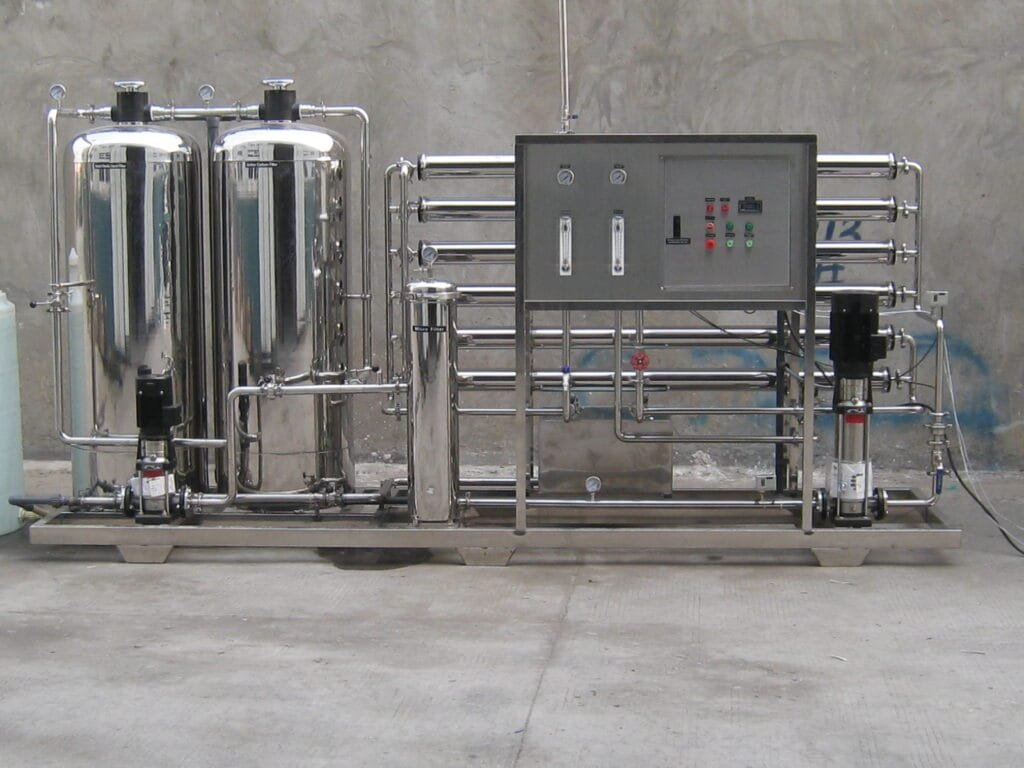
Adopts high desalination rate reverse osmosis membrane, the core component of ro water treatment equipment, effectively filters heavy metals, bacteria, sediment and scale, delivering stable purified water quality for long-term operation.
2. Full-Automatic Operation for Industrial RO Water Treatment System
Built-in auto flushing, low/high pressure protection and water shortage alarm modules. This ro water treatment unit reduces manual intervention and lowers maintenance labor costs for commercial & factory usage.
3. Customizable Capacity Fits All RO Water Treatment Demands
Support customized 0.25T–100T per hour output. Our ro water treatment solution matches residential drinking water, hotel water supply, food beverage processing and pharmaceutical industrial water requirements.
4. Energy-Saving & Low Waste Water Design
Optimized pipeline and pressure structure cuts power consumption of the ro water treatment machine. Adjustable wastewater ratio improves water utilization rate to save running expenses.
5. Corrosion-Resistant Food-Grade Material
Main frame uses stainless steel, pipeline adopts UPVC anti-corrosion fittings. The whole ro water treatment equipment meets international drinking water safety standards, durable for harsh raw water environments.
6. Simple Structure & Easy Daily Maintenance
Modular integrated design of the ro water treatment system allows quick filter element and membrane replacement without professional technicians, greatly shortening downtime.
7. Intelligent Control Panel with Real-Time Monitoring
Digital display shows water pressure, water yield and running status of the ro water treatment plant, convenient for operators to check working conditions anytime.
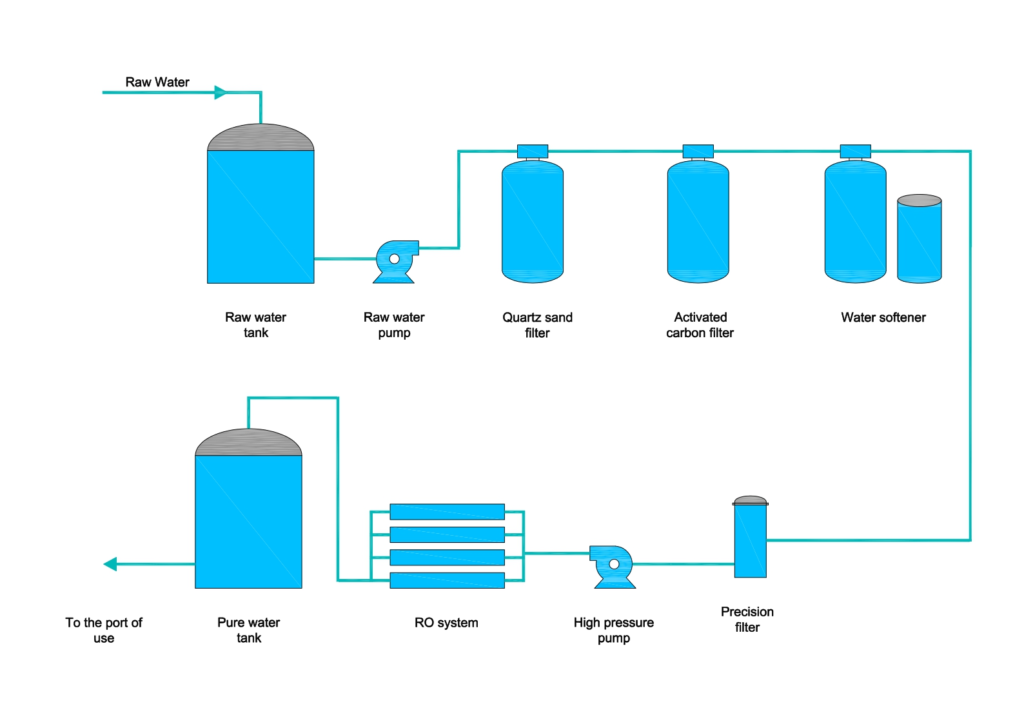
Working Principle
FAQs
Q: What types of industrial water problems can your treatment equipment solve?
A:Our industrial water treatment equipment is designed for diverse industrial wastewater and raw water purification scenarios. It effectively removes suspended solids, heavy metals, oil stains, organic pollutants, calcium and magnesium ions, and harmful microorganisms. It is widely applicable for boiler feed water treatment, circulating water purification, industrial wastewater reuse, sewage standard discharge, and underground/river raw water filtration for manufacturing, chemical, food and beverage, textile, mining and other industries.
Q: What is the water treatment capacity of your equipment? Is it customizable?
A: We provide full-range configurable water treatment capacity from 1m³/h to 500m³/h to meet different production scales. All equipment supports one-stop customized design according to clients’ actual water quality test reports, water volume demand and industrial emission standards. We can adjust equipment configuration, filtration precision and process flow to fit special working conditions, ensuring optimal treatment efficiency and cost performance.
Q: What international standards does your equipment comply with?
A: Our industrial water treatment equipment strictly follows international industry specifications and has passed multiple global certifications. All products comply with ISO 9001 quality management system standards, and meet local environmental discharge and water reuse standards for most overseas regions. The core filter materials, control systems and pressure components conform to EU CE certification requirements, ensuring safe, stable and standard-compliant operation in global industrial projects.
Q: Can the equipment realize wastewater recycling and reuse?
A: Yes. Our tailored industrial water treatment systems can efficiently treat industrial sewage and wastewater to reach factory reuse standards. The treated water can be reused for production circulation, equipment cooling, factory cleaning and other links, greatly reducing industrial water consumption and water cost, and helping enterprises achieve green production and meet environmental protection assessment requirements.